Knowledge 25 May 2026
Packaging Systems in Supplement Manufacturing
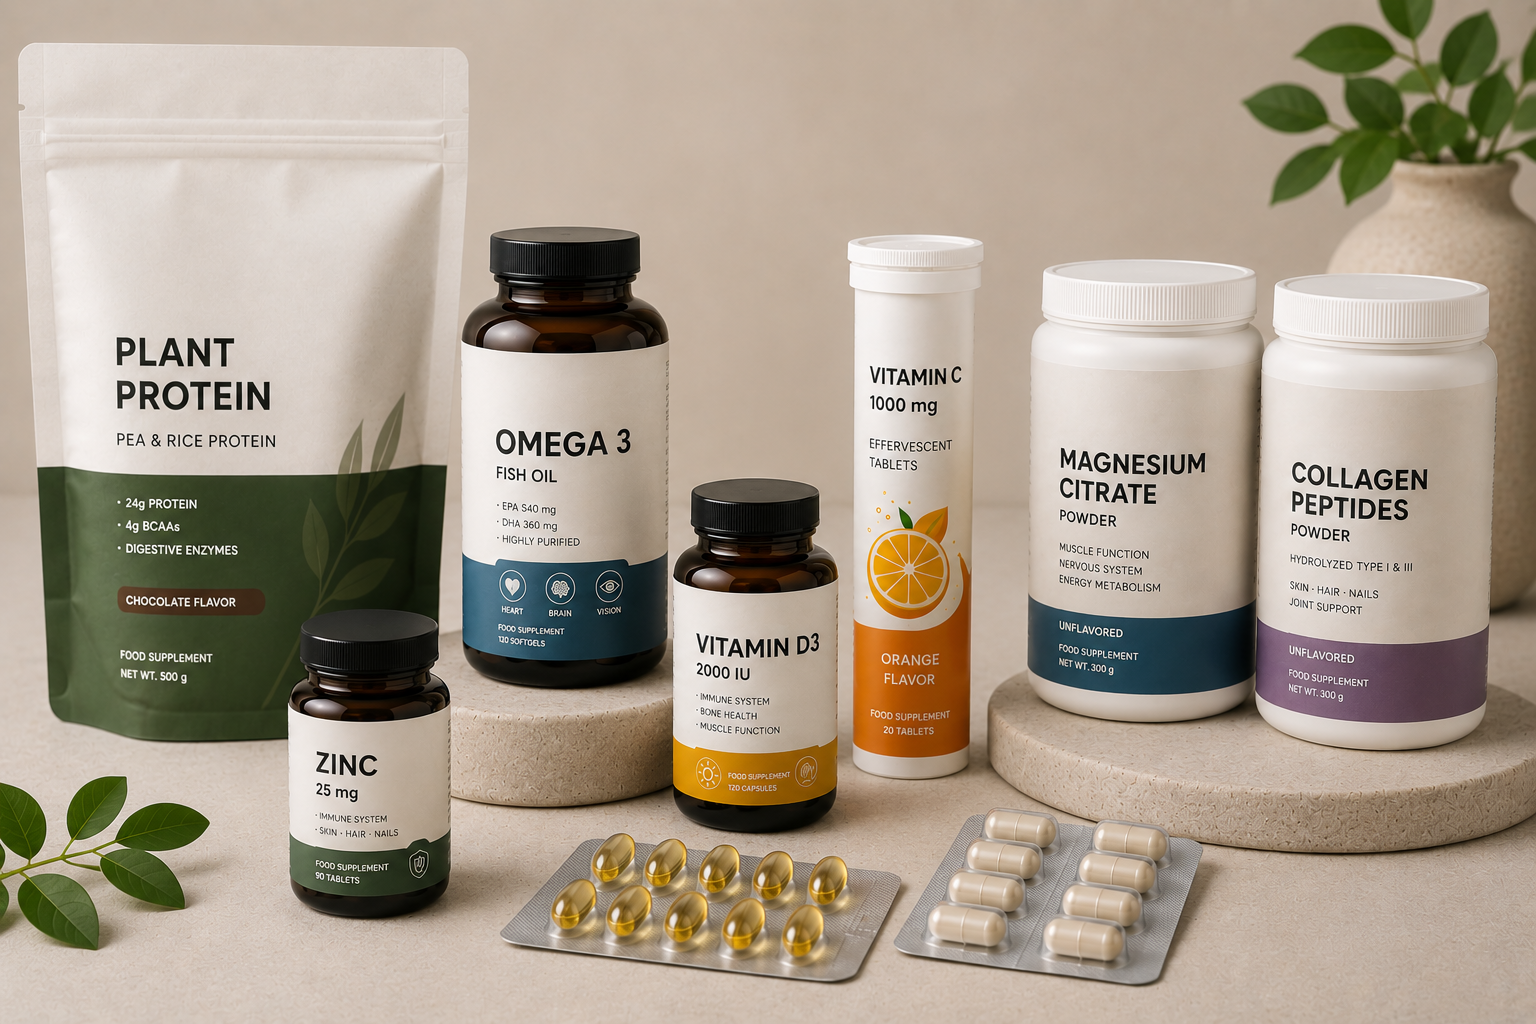
Packaging plays a far greater role in supplement manufacturing than many brands initially expect. Beyond visual presentation, packaging directly affects product stability, shelf life, moisture protection, transport safety, and overall consumer perception.
In European supplement manufacturing, packaging must work together with formulation and storage conditions to help maintain product quality throughout its lifecycle. The right packaging system helps protect supplements from environmental exposure while also supporting compliance, functionality, and brand positioning.
At PharmaEurope, packaging selection is integrated early in product development to ensure that each product format receives appropriate protection and presentation.
This article explains how packaging protection systems support supplement stability, what packaging formats are commonly used for different dosage forms, and how packaging also contributes to marketing and consumer experience.
Why Packaging Matters in Supplement Manufacturing
Packaging is not only a container — it is part of the product stability system.
In supplement manufacturing, packaging helps protect products from:
- moisture exposure
- oxygen exposure
- light sensitivity
- contamination risks
- transport and handling damage
Without proper packaging, even a well-designed formulation may lose stability over time.
This is particularly important for moisture-sensitive supplements such as:
- effervescent tablets
- powder supplements
- probiotics
- botanical extracts
- hygroscopic minerals
Packaging decisions therefore directly influence achievable shelf life and product quality.
Packaging Protection Systems Used in Supplement Manufacturing
Different supplement products require different protection systems depending on formulation sensitivity, dosage form, and storage conditions.
Desiccant Systems and Moisture Control
Moisture is one of the most common causes of supplement instability.
To reduce humidity exposure, manufacturers commonly use:
- silica gel sachets
- integrated desiccant stoppers
- moisture-absorbing caps
- controlled barrier packaging materials
These systems help maintain stability by reducing moisture inside the packaging environment.
Desiccant stoppers are particularly important for effervescent tablets, where even minimal humidity exposure may trigger premature reactions.
Induction Seals and Shrink Sleeves
Sealing systems provide both protection and tamper evidence.
Common systems include:
Induction seals
Applied under bottle caps to help reduce:
- moisture entry
- oxygen exposure
- contamination risks
They also provide product integrity during transport and storage.
Shrink sleeves and shrink bands
Used to:
- provide tamper evidence
- improve transport protection
- support product presentation
These systems are widely used across capsule, tablet, powder, and softgel packaging.
Barrier Packaging Materials
Certain supplement products require packaging materials with stronger protective properties.
Examples include:
- multilayer doypacks
- foil barrier systems
- blister packaging
- amber glass bottles
Barrier materials help reduce:
- oxygen transmission
- moisture penetration
- UV light exposure
This is especially important for sensitive formulations and products with longer shelf-life expectations.
Packaging Solutions by Dosage Form
Different supplement formats require different packaging approaches.
Capsules
Capsules are commonly packed in:
- PET bottles
- HDPE bottles
- amber glass bottles
- blister packaging
Moisture control is particularly important for capsule shell stability, especially in humid environments.
Depending on formulation sensitivity, desiccants and induction seals may be recommended.
Related: Private Label Capsule Manufacturing in Europe
Tablets
Tablet packaging depends on:
- coating type
- hygroscopicity
- stability requirements
- transport conditions
Common solutions include:
- bottles
- blisters
- induction-sealed containers
Film-coated tablets may provide improved environmental resistance compared to uncoated formats.
Related: Private Label Tablet Manufacturing in Europe
Effervescent tablets are among the most moisture-sensitive supplement formats.
Because effervescent reactions can be triggered by humidity exposure, packaging systems must provide highly controlled conditions.
See private label effervescent tablet manufacturing for how the tube and desiccant cap are built into the formula.
Common solutions include:
- moisture-protected tubes
- integrated desiccant stoppers
- sealed transport systems
Packaging integrity is critical for maintaining product stability throughout shelf life.
Related: Private Label Effervescent Tablets Manufacturing
Powder supplements require packaging systems that help reduce:
- clumping
- moisture absorption
- segregation
- contamination risks
Common packaging formats include:
- powder jars
- doypacks
- stick packs
- induction-sealed containers
Additional protection systems may include:
- silica gel systems
- barrier materials
- scoop protection inserts
Related: Private Label Powder Supplements in Europe
Softgels
Softgel formulations are often sensitive to:
- temperature
- oxygen exposure
- oil oxidation
- light exposure
Packaging solutions may include:
- opaque bottles
- amber packaging
- blister systems
- oxygen-reducing packaging environments
Packaging selection helps support oil stability and capsule integrity over time.
See private label softgel manufacturing for how oxygen and light protection are chosen for oil-based fills.
Packaging as a Marketing and Branding Tool
Packaging is not only functional — it also influences how consumers perceive a supplement product.
In competitive supplement markets, packaging contributes to:
- shelf visibility
- premium appearance
- brand recognition
- perceived product quality
- consumer convenience
Brands often select packaging formats based not only on technical requirements, but also on target audience and market positioning.
Packaging customization may include:
- colored PET bottles
- amber glass packaging
- printed doypacks
- carton boxes
- custom labels
- premium finishing elements
The right packaging combination helps create both product protection and stronger visual identity.
Choosing the Right Packaging for Supplement Products
Selecting suitable packaging requires balancing several factors:
- formulation sensitivity
- shelf-life expectations
- dosage form
- transport conditions
- target market
- branding strategy
- storage environment
A packaging format that works well for one supplement type may not be suitable for another.
For example:
- effervescent tablets require strong moisture protection
- powders often require barrier packaging
- softgels may require light and oxygen protection
Packaging decisions should therefore be aligned early with product development and manufacturing planning.
How PharmaEurope Supports Packaging Selection?
At PharmaEurope, packaging selection is integrated into supplement development from the early stages of production planning.
Packaging support includes:
- packaging compatibility evaluation
- moisture-sensitive product considerations
- dosage-form-specific packaging selection
- packaging component recommendations
- labeling and sizing guidance
- packaging customization options
Available packaging formats include:
- PET bottles
- colored PET bottles
- amber glass bottles
- powder jars
- doypacks
- effervescent tubes
- carton boxes
- leaflets and inserts
This helps ensure that packaging supports both product stability and market positioning.
Final Takeaway
In supplement manufacturing, packaging is far more than a visual component.
Effective packaging systems help protect supplements from moisture, oxygen, light, contamination, and transport-related risks while also supporting shelf life, compliance, and brand presentation.
Different dosage forms require different protection strategies, which is why packaging selection should always be aligned with formulation characteristics and stability expectations.
When packaging, product stability, and branding work together, supplement products are better positioned for long-term quality and market success.
Thinking about your own product? Tell us the format, the active and its dose, and how many units you need for the first run. Ready-made formulas start from 100 units, and we reply within 24 hours, Monday to Friday.
Written by the PharmaEurope manufacturing team at the ISO 22000-certified plant in the European Union. Last reviewed 23 September 2026.
Where this is made
Request a quoteReady-made formulas from 100 units. We reply within 24 hours, Monday to Friday.
Read next
 Private label vitamin D3 + K2 and vegan vitamin D3PharmaEurope makes private label vitamin D3 + K2 in softgels, tablets and effervescent tubes of 20, and vegan vitamin D3 from algae, at our EU plant. White label starts from 100 units, standard own-label runs from 500 bottles (500 pcs for stock softgels), your own brand on a ready-made formula is in production from 2 […]27 October 2026
 Why vitamin D is a strong first product for your supplement brandVitamin D is a strong first product for a new supplement brand because the ingredient is well known to buyers, the product is taken every day and the EU allows seven authorised health claims for it. PharmaEurope manufactures private label vitamin D in its certified EU plant: white label on a ready-made formula from 100 […]27 October 2026
 What vitamin D does and what an EU label may sayIn the EU, what vitamin D does may be stated on a supplement label only in the seven authorised health claims of Regulation (EU) No 432/2012, for example "Vitamin D contributes to the maintenance of normal bones", and only when a daily serving supplies at least 15 % of the 5 µg NRV, which is […]27 October 2026