Knowledge 5 May 2026
Excipients in Supplement Manufacturing: Types, Functions and Formulation Role
Excipients in supplement manufacturing play a critical role in ensuring product quality, stability, and production efficiency.
While active ingredients define the intended function of a supplement, excipients determine how effectively that product can be produced, stored, and used.
In the European Union, where supplements must meet strict safety and quality standards, excipient selection is an essential part of formulation development. Poor excipient choices can lead to production issues, inconsistent dosing, stability problems, or reduced consumer acceptance.
This article explains what excipients are, how they function across different supplement formats, and why they are a key component of successful supplement manufacturing.
What are excipients in supplements?
Excipients are substances added to a formulation to support the manufacturing process and improve the performance of the final product. Unlike active ingredients, excipients do not provide the primary nutritional or physiological effect. However, they are essential for ensuring that the product can be manufactured consistently and performs as expected throughout its shelf life.
Depending on the dosage form, excipients can influence:
- powder flow and capsule filling
- tablet compression and disintegration
- product stability and shelf life
- solubility and taste
- overall consumer usability
In practice, most supplement formulations require a combination of excipients to achieve optimal performance.
Main types of excipients and their functions
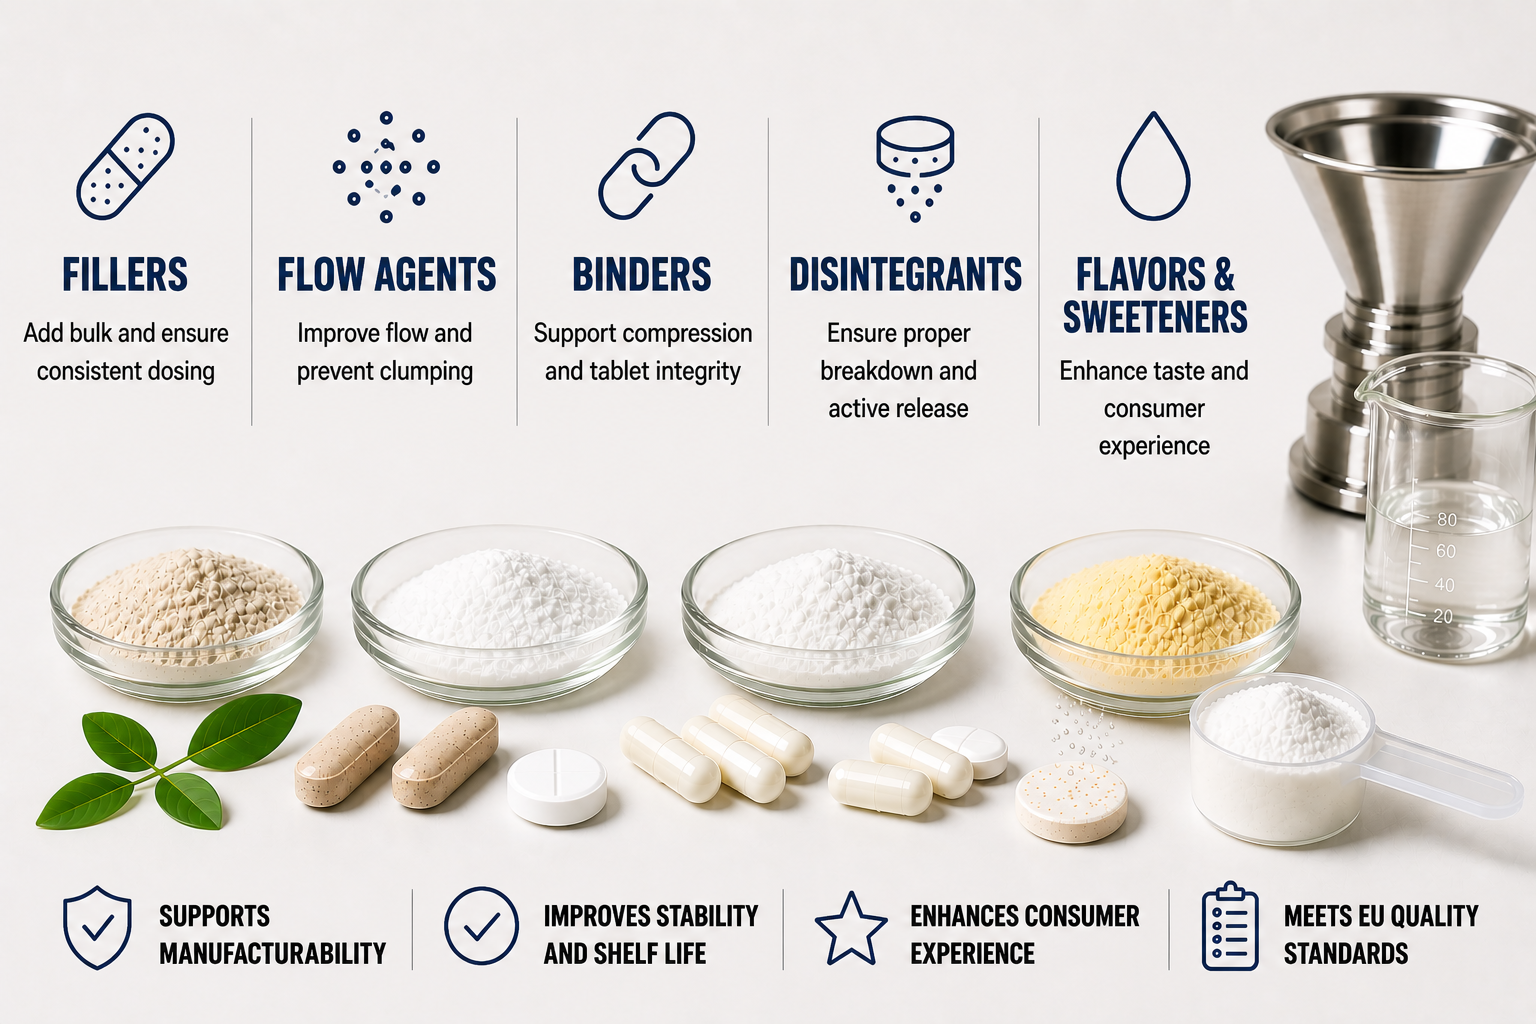
Excipients can be grouped based on their functional role in the formulation.
Fillers and bulking agents
Fillers are used to increase the volume of a formulation when active ingredient dosage is low. Common examples include microcrystalline cellulose (MCC) and calcium hydrogen phosphate. These excipients help ensure consistent dosing and allow capsules or tablets to reach a practical size.
Flow agents and anti-caking agents
Flow agents improve the movement of powders during manufacturing processes such as capsule filling or tableting. Examples include silicon dioxide and magnesium stearate. They help prevent clumping and ensure uniform distribution of ingredients.
Binders and compression aids
Binders are used primarily in tablet formulations to hold ingredients together during compression.They influence tablet hardness, mechanical stability, and overall production efficiency.
Disintegrants
Disintegrants ensure that tablets break down properly after ingestion, allowing active ingredients to be released. Without proper disintegration, product effectiveness may be reduced.
Flavours, sweeteners, and functional additives
In powder and effervescent products, excipients also contribute to consumer experience. These may include flavour systems, sweeteners such as stevia or sucralose, and acidity regulators such as citric acid. These components improve taste, solubility, and overall usability.
How excipients are used in real supplement manufacturing
In practice, excipients are selected based on functionality rather than simply filling space. In EU supplement manufacturing, their role is closely linked to formulation performance, production efficiency, and final product quality.
Capsule formulations
For capsule formulations, excipients are primarily used to ensure:
- consistent filling
- stable powder flow
- accurate dosing
Common examples include microcrystalline cellulose (MCC) as a bulking and flow-stabilizing agent, as well as magnesium stearate and silicon dioxide to improve powder flow. Calcium-based fillers are often used to optimize density and capsule fill weight.
Powder formulations
In powder supplements, excipients play a key role in product usability.
They are used to improve:
- dosing consistency
- taste and mouthfeel
- solubility
Carriers such as maltodextrin help stabilize the formulation, while acids, flavours, and sweeteners are used to improve consumer experience—especially in products containing minerals or amino acids.
Formulation approach
Rather than applying a fixed approach, excipient selection depends on several factors:
- active ingredient load
- dosage form
- hygroscopicity
- target serving size
For example, capsule formulations must consider size limitations, while powders must balance serving size, solubility, and palatability.
Optimization instead of overuse
A key aspect of professional formulation is avoiding unnecessary excipient use.
Overuse of fillers or functional agents can:
- negatively affect product quality
- increase cost
- reduce consumer acceptance
Instead, excipients are optimized to support manufacturability, stability, and overall product performance.
Flexible formulation approach
In addition, excipient selection can be adapted based on specific project requirements. Depending on formulation goals, target markets, or customer preferences, alternative excipient systems can be evaluated to ensure both technical performance and product positioning are aligned.
Manufacturing perspective
At PharmaEurope, excipient selection is evaluated during formulation development to ensure both product stability and production feasibility.
Excipients across different supplement formats
The role of excipients varies depending on the dosage form.
Capsules
Excipients improve powder flow, ensure consistent fill weight, and support capsule integrity. Capsule size limitations require careful balancing between active ingredients and excipients.
See private label capsule manufacturing, formula to finished bottle.
Tablets
Tablet formulations rely heavily on excipients. They require binders for compression, disintegrants for release, and lubricants for manufacturing efficiency.
What that means in production, including coating and packing, is on our private label tablet manufacturing page.
Powder supplements
Powders require excipients that support flowability, solubility, taste, and stability. They are especially important for consumer experience.
Here is private label powder manufacturing, minimum order from 300 kg.
Effervescent tablets
Effervescent formulations depend on functional excipients such as acids and carbonates to create the reaction. These systems also require strict moisture control and compatible packaging.
Key formulation considerations when selecting excipients
In excipients in supplement manufacturing, selecting the right combination is essential for both product performance and manufacturability. Selecting the right excipients involves balancing multiple factors:
- active ingredient properties
- dosage form requirements
- manufacturing process limitations
- target shelf life
- packaging compatibility
Excipients must also be compatible with each other and with active ingredients to ensure long-term stability.
Common risks and mistakes
Improper excipient selection can lead to:
- inconsistent dosing
- poor tablet performance
- clumping in powders
- reduced stability and shelf life
- unnecessary product size or cost
A common mistake is overusing excipients without a clear functional purpose. Effective formulation focuses on optimization rather than maximization.
Final takeaway
Understanding excipients in supplement manufacturing helps brands develop more stable and efficient supplement products. Excipients are a fundamental part of supplement manufacturing, directly influencing product quality, stability, and production efficiency.
While they do not provide the primary function of a supplement, they enable the product to be manufactured consistently and perform as intended.
Understanding the role of excipients helps brands make better formulation decisions and avoid common production challenges.
Next step
If you are developing a supplement for the EU market, early evaluation of excipient selection, formulation compatibility, and manufacturing feasibility can significantly improve product performance and production outcomes. For more detailed guidance on different supplement formats and manufacturing approaches, explore our full blog section covering capsules, tablets, powders, and effervescent products.
Thinking about your own product? Tell us the format, the active and its dose, and how many units you need for the first run. Ready-made formulas start from 100 units, and we reply within 24 hours, Monday to Friday.
Written by the PharmaEurope manufacturing team at the ISO 22000-certified plant in the European Union. Last reviewed 5 May 2026.
Where this is made
Request a quoteReady-made formulas from 100 units. We reply within 24 hours, Monday to Friday.
Read next
 Private label vitamin D3 + K2 and vegan vitamin D3PharmaEurope makes private label vitamin D3 + K2 in softgels, tablets and effervescent tubes of 20, and vegan vitamin D3 from algae, at our EU plant. White label starts from 100 units, standard own-label runs from 500 bottles (500 pcs for stock softgels), your own brand on a ready-made formula is in production from 2 […]27 October 2026
 Why vitamin D is a strong first product for your supplement brandVitamin D is a strong first product for a new supplement brand because the ingredient is well known to buyers, the product is taken every day and the EU allows seven authorised health claims for it. PharmaEurope manufactures private label vitamin D in its certified EU plant: white label on a ready-made formula from 100 […]27 October 2026
 What vitamin D does and what an EU label may sayIn the EU, what vitamin D does may be stated on a supplement label only in the seven authorised health claims of Regulation (EU) No 432/2012, for example "Vitamin D contributes to the maintenance of normal bones", and only when a daily serving supplies at least 15 % of the 5 µg NRV, which is […]27 October 2026