Knowledge 15 July 2026
Probiotic Ingredients in Food Supplements
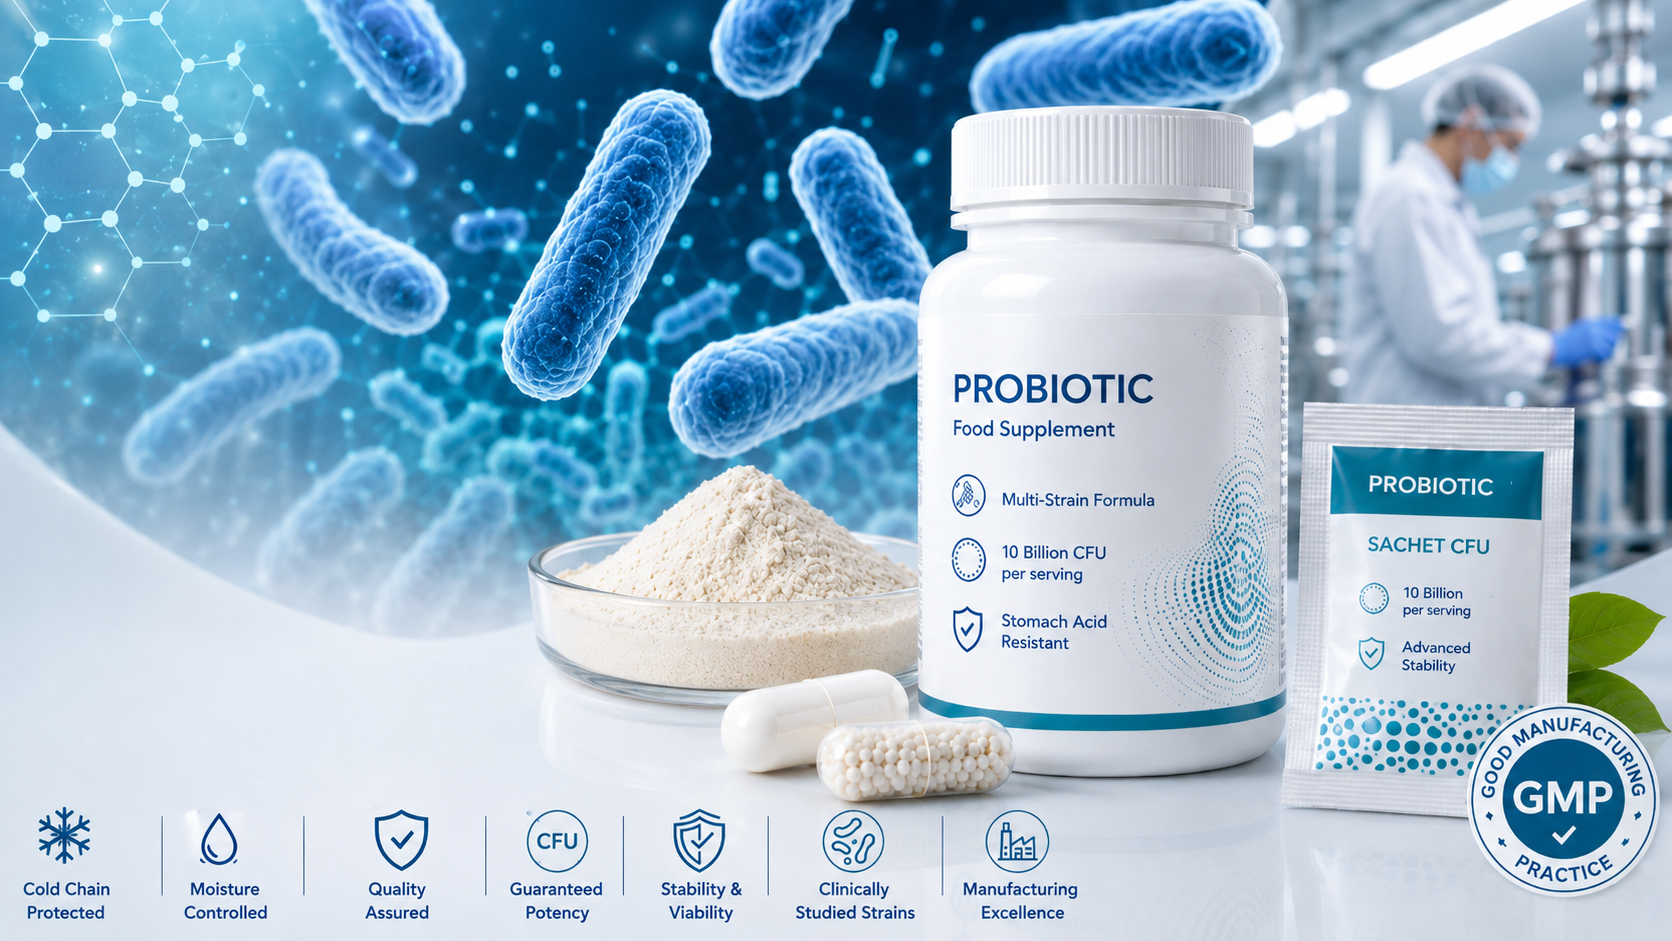
Probiotic ingredients represent one of the most technically challenging categories used in modern food supplements. Unlike vitamins, minerals, amino acids, or botanical extracts, probiotics are living microorganisms whose quality depends not only on their identity but also on how they are manufactured, handled, packaged, and stored.
Developing a successful probiotic supplement involves far more than selecting a high CFU number. Manufacturers must evaluate strain identity, stability, compatibility with other ingredients, dosage form, packaging systems, and expected shelf life to ensure consistent product quality.
This guide explains how probiotic ingredients are produced, how strains differ, what CFU really means, and the key manufacturing considerations involved in developing probiotic food supplements.
What Are Probiotic Ingredients?
Probiotic ingredients are standardized raw materials containing carefully selected live microorganisms supplied for use in food supplement manufacturing.
Most commercial probiotic ingredients are produced through controlled fermentation processes and are stabilized before being incorporated into capsules, powders, tablets, or sachets.
Unlike traditional nutritional ingredients, probiotics remain biologically active throughout their shelf life, making formulation and storage considerably more demanding.
Common probiotic microorganisms used in food supplements include:
- Lacticaseibacillus
- Lactiplantibacillus
- Bifidobacterium
- Bacillus
- Saccharomyces boulardii (a probiotic yeast)
Each ingredient possesses unique characteristics regarding stability, processing, moisture sensitivity, and formulation compatibility.
How Probiotic Ingredients Are Produced
Although probiotic supplements appear simple from the outside, the ingredients undergo a highly controlled manufacturing process before reaching supplement manufacturers.
A simplified production process typically includes:
- Selection of the probiotic strain
- Controlled fermentation
- Separation and concentration
- Freeze-drying (lyophilization) or alternative stabilization
- Quality testing
- Packaging as a probiotic raw material
- Incorporation into finished food supplements
Freeze-drying removes water while helping preserve viable microorganisms, allowing probiotic ingredients to remain stable during transport and manufacturing.
Understanding Probiotic Classification
Every probiotic ingredient is identified using three different levels.
| Classification | Example |
|---|---|
| Genus | Lacticaseibacillus |
| Species | rhamnosus |
| Strain | GG |
For example:
Lacticaseibacillus rhamnosus GG
The strain designation is particularly important because different strains within the same species are distinct raw materials with their own technical documentation and manufacturing characteristics.
Manufacturers therefore evaluate probiotic ingredients primarily at the strain level rather than by species name alone.
Common Probiotic Ingredients Used in Food Supplements
| Genus | Common Species | Typical Supplement Formats | Stability Characteristics |
|---|---|---|---|
| Lacticaseibacillus | Various strains | Capsules, Powders | Moisture sensitive |
| Bifidobacterium | Various strains | Capsules, Sachets | Highly moisture sensitive |
| Bacillus | B. coagulans, B. subtilis | Capsules, Tablets | Naturally more stable |
| Saccharomyces | S. boulardii | Capsules | Moderate stability |
Freeze-Dried vs Spore-Forming Probiotics
Not all probiotic ingredients behave the same during manufacturing.
Many traditional probiotic bacteria are supplied as freeze-dried cultures that require careful protection from heat and moisture throughout production and storage.
Some probiotic ingredients, particularly selected Bacillus species, naturally produce spores. These spore-forming microorganisms are generally more resistant to environmental conditions and may offer greater manufacturing robustness in certain formulations.
The most suitable ingredient depends on the intended dosage form, storage conditions, packaging system, and overall product concept.
What Does CFU Mean?
Probiotic potency is expressed as CFU (Colony Forming Units).
CFU represents the number of viable microorganisms present in a probiotic ingredient or finished product.
Typical supplement formulations may contain:
- 1 Billion CFU
- 5 Billion CFU
- 10 Billion CFU
- 20 Billion CFU
- 50 Billion CFU
However, a higher CFU value does not automatically indicate a superior product.
Manufacturers evaluate CFU alongside strain identity, formulation compatibility, stability data, and expected shelf life.
CFU values are generally declared per recommended daily serving, although labeling practices may vary depending on product design.
Why Shelf-Life Matters
Unlike vitamins or minerals, probiotic ingredients naturally lose viability over time.
To compensate for this, manufacturers may incorporate an overage, meaning additional viable microorganisms are included during production so the declared CFU level remains available at the end of the product's intended shelf life.
The required overage depends on:
- probiotic strain
- moisture exposure
- storage temperature
- packaging system
- dosage form
- intended shelf life
Single-Strain vs Multi-Strain Formulations
Probiotic supplements may contain a single probiotic strain or multiple strains combined within one formulation.
Single-strain products focus on one identified microorganism, while multi-strain formulations combine several strains with different technical characteristics.
From a manufacturing perspective, combining multiple strains requires careful evaluation of ingredient compatibility, blending conditions, stability, and packaging requirements.
Manufacturing Challenges
Because probiotics remain living microorganisms, manufacturing conditions require special attention.
Manufacturers typically evaluate:
- moisture exposure
- processing temperature
- blending sequence
- compression forces
- encapsulation conditions
- ingredient compatibility
- storage conditions
- packaging selection
These factors help support probiotic stability from production through to the end of shelf life.
Packaging and Storage
Packaging plays a major role in probiotic stability.
Depending on the formulation, manufacturers may select:
- moisture-resistant bottles
- silica gel desiccants
- blister packaging
- high-barrier containers
- individual sachets
Manufacturers also consider bottle opening frequency, consumer handling, and humidity exposure after opening when selecting packaging systems.
Read more: Packaging Systems in Supplement Manufacturing
Documentation Manufacturers Review
Before selecting a probiotic ingredient, manufacturers typically evaluate:
- strain designation
- Certificate of Analysis (CoA)
- Product Specification
- declared CFU
- stability studies
- recommended storage conditions
- allergen status
- Non-GMO declaration
- microbiological testing
These documents help verify ingredient identity and support consistent manufacturing.
Probiotics in Different Dosage Forms
Capsules
Capsules remain the most common dosage form because they provide excellent formulation flexibility while helping protect moisture-sensitive ingredients.
Our own probiotic work runs the same way: see capsule manufacturing, including delayed-release shells.
Tablets
Only selected probiotic ingredients are suitable for tablet manufacturing because compression forces may reduce viability.
Powders
Powder formulations are frequently used for probiotics intended for direct consumption or mixing with liquids.
Sachets
Single-dose sachets reduce repeated exposure to environmental moisture after opening and are commonly selected for probiotic formulations.
See single-dose sachet manufacturing for moisture-sensitive actives.
Ingredient Snapshot
| Category | Probiotic Ingredients |
|---|---|
| Source | Controlled fermentation |
| Living microorganisms | Yes |
| Typical Forms | Capsules, Powders, Tablets, Sachets |
| Moisture Sensitivity | High (varies by strain) |
| Packaging Importance | Very High |
| Manufacturing Complexity | High |
Did You Know?
- Not all probiotic ingredients require refrigerated storage.
- Different strains within the same species may have very different stability characteristics.
- Freeze-drying is one of the most common stabilization technologies used for probiotic ingredients.
- Packaging selection can significantly influence long-term probiotic stability.
Choosing the Right Probiotic Ingredient
Manufacturers typically evaluate:
✓ strain identity
✓ CFU level
✓ stability profile
✓ dosage form
✓ ingredient compatibility
✓ packaging system
✓ supplier documentation
✓ shelf-life objectives
Selecting the appropriate probiotic ingredient during early product development helps support stable manufacturing and consistent product quality.
Final Takeaway
Probiotic ingredients differ fundamentally from many other food supplement ingredients because they remain living microorganisms throughout their intended shelf life.
Successful probiotic supplements depend on much more than CFU numbers. Strain identity, stability, manufacturing conditions, packaging systems, and storage all contribute to the quality of the finished product.
Understanding these technical factors allows manufacturers to develop probiotic formulations that remain stable and consistent from production to the end of shelf life.
FAQ
What does CFU mean?
CFU (Colony Forming Units) indicates the number of viable microorganisms present in a probiotic ingredient or finished supplement.
Why is the probiotic strain important?
Different strains within the same species are unique ingredients with their own technical characteristics and supporting documentation.
What is the difference between species and strain?
A species is a biological classification, while a strain is a uniquely identified microorganism within that species.
Are probiotics suitable for tablets?
Some strains are suitable, but manufacturers must evaluate whether compression forces could affect stability.
Do probiotics require special packaging?
Many probiotic formulations benefit from moisture-resistant packaging and desiccants to help maintain stability during storage.
Can probiotics be used in capsules, powders, and sachets?
Yes. Probiotic ingredients are commonly formulated into capsules, powders, tablets, and sachets depending on the product concept.
Thinking about your own product? Tell us the format, the active and its dose, and how many units you need for the first run. Ready-made formulas start from 100 units, and we reply within 24 hours, Monday to Friday.
Written by the PharmaEurope manufacturing team at the ISO 22000-certified plant in the European Union. Last reviewed 15 July 2026.
Where this is made
Request a quoteReady-made formulas from 100 units. We reply within 24 hours, Monday to Friday.
Read next
 Private label vitamin D3 + K2 and vegan vitamin D3PharmaEurope makes private label vitamin D3 + K2 in softgels, tablets and effervescent tubes of 20, and vegan vitamin D3 from algae, at our EU plant. White label starts from 100 units, standard own-label runs from 500 bottles (500 pcs for stock softgels), your own brand on a ready-made formula is in production from 2 […]27 October 2026
 Why vitamin D is a strong first product for your supplement brandVitamin D is a strong first product for a new supplement brand because the ingredient is well known to buyers, the product is taken every day and the EU allows seven authorised health claims for it. PharmaEurope manufactures private label vitamin D in its certified EU plant: white label on a ready-made formula from 100 […]27 October 2026
 What vitamin D does and what an EU label may sayIn the EU, what vitamin D does may be stated on a supplement label only in the seven authorised health claims of Regulation (EU) No 432/2012, for example "Vitamin D contributes to the maintenance of normal bones", and only when a daily serving supplies at least 15 % of the 5 µg NRV, which is […]27 October 2026